Petrochemical & Power Fasteners: 304/316 Stainless vs Nickel-Based Alloys
Petrochemical & Power Fasteners: 304/316 Stainless vs. Nickel-Based Alloys
On a petrochemical or power generation project, the material decision for high-performance fasteners is usually settled before the flange schedule, the steam line class and the goods-in inspection plan are finalised. Choose 304/316 stainless steel where the joint is correct for it, and nickel-based high-temperature alloys where the joint demands them, and the bolting disappears into the background. Choose by default, in either direction, and the cost reappears later as rejected deliveries, re-torque campaigns or unplanned replacement.
This guide compares both material families head to head for petrochemical and power generation service, and maps them onto the product forms, strength grades, thread tolerance classes, surface treatments, standards and acceptance criteria that a buyer actually has to write onto a purchase order.
Short answer: For general corrosive duty, ambient and standard process conditions, 304/316 austenitic stainless fasteners in A2-70, A2-80, A4-70 or A4-80 grades cover the requirement. Where the working condition combines high temperature with high tensile load and demands high-temperature resistance and anti-fatigue performance, the specification moves to nickel-based and high-alloy options such as A286 ALLOY 660, ALLOY 718 and ALLOY 80A, or to duplex and high-molybdenum grades such as UNS S32205, 316Ti (1.4571) and 904L (1.4539). UHC (Jiaxing Union Hardware Co., Ltd.) manufactures both families to ISO, DIN, ASTM, ASME, ANSI and JIS standards, in sizes from M2 to M160.
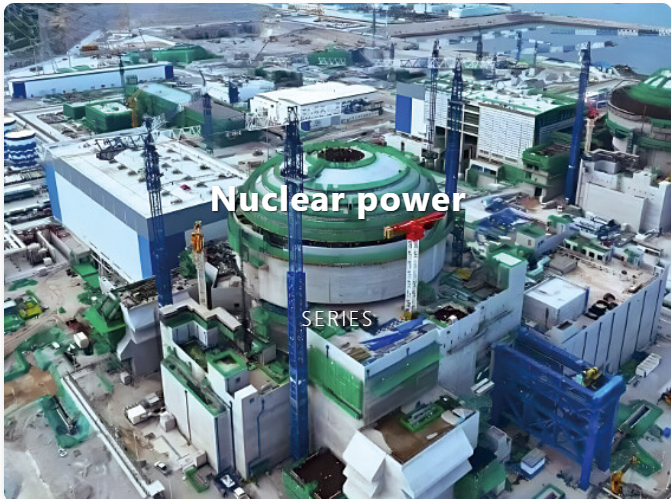
A single power generation or petrochemical site holds ambient, corrosive and high-temperature joints side by side — which is why material selection is made joint by joint, not plant by plant.
What the Material Decision Has to Solve
A petrochemical complex or a power station is not one environment. The same site contains normal-temperature structural connections, acid and alkali corrosive zones, high-temperature process and steam lines, seawater-exposed equipment on coastal sites, high-vibration machinery skids and joints carrying high tensile load. Fasteners in these locations perform the same physical function — mechanical connection, fastening, locking, anti-loosening and fixed assembly between mechanical components — but the material that survives one location may be the wrong purchase in another.
The decision problem is therefore not “stainless or alloy”. It is a four-part question that has to be answered for every joint type on the project:
- Which working condition dominates — normal temperature, high temperature, seawater corrosion, acid and alkali corrosive environment, high vibration, or high tensile load?
- Which material family meets that condition without unnecessary cost?
- Which strength grade, product form and thread tolerance class physically fits the joint?
- Which standard, surface treatment, inspection regime and certificate package proves it at goods-in?
Most failures in this process are not metallurgical; they are documentary and dimensional. A quoted strength grade that does not match the specification, a 6H nut supplied where 3B thread tolerance was required, a natural finish delivered against a Dacromet coating requirement, or a shipment without the agreed material certificate creates a rejection at the gate regardless of how good the steel is.
Industry Background: Why the Split Between Stainless and Alloy Matters More Now
Demand for high-performance fasteners continues to scale with industrial investment. The global industrial fasteners market was valued at USD 103.9 billion in 2025 and is projected to reach USD 153.7 billion by 2033, according to Grand View Research. The same research shows Asia Pacific holding a 45.1% revenue share in 2025, metal fasteners accounting for 91.0% of the market, and externally threaded fasteners — bolts, screws and studs — generating 48.1% of global fastener revenue in 2025.
The high-alloy end of that market is tracked separately because it behaves differently. Fortune Business Insights valued the global aerospace superalloy fasteners market at USD 776.7 million in 2024. The Insight Partners projects the wind power fastener market to reach USD 14.68 billion in 2025, against a Global Wind Energy Council outlook of wind turbine capacity growing from 1,100 GW in 2025 to over 2,400 GW by 2030. In marine and heavy industry, China’s new shipbuilding orders rose 59.0% year on year in Q1 2024, according to the China Association of the National Shipbuilding Industry.
Compliance pressure is moving in the same direction. Fasteners for pressure equipment in the EU must comply with the Pressure Equipment Directive (PED) 2014/68/EU. ISO 3506-1:2020 specifies the mechanical properties of corrosion-resistant stainless steel bolts, screws and studs. The EN 14399 series governs high-strength structural bolting assemblies for preloading, AS9100 sets quality management requirements for aerospace, space and defence organisations, and ISO/IEC 17025 is the recognised benchmark for testing and calibration laboratory competence.
These application scenarios are common in Germany, Japan, South Korea and Italy, and they are the markets where specification discipline is tightest. That combination — growing demand, harder compliance requirements and buyers comparing two material families on the same drawing — is exactly why the 304/316 versus nickel-based alloy decision deserves a structured method rather than a default.
Material Options Available for Petrochemical and Power Generation
The material list behind UHC’s fastener specifications covers 304, 316, UNS S32205, 1.4571, 316Ti, 1.4529, UNS N08926, 1.4980, A286 ALLOY 660, 1.4539, 904L, 2.4952, 2.4668, ALLOY 80A, ALLOY 718, 1.4006, S41000, 1.4462, 1.4410, UNS S32750 and 2507. For a project buyer, that long list is easier to use when it is grouped by the job it does.
Austenitic stainless steel: 304 and 316 (A2 and A4 grades)
304 and 316 are the workhorses of petrochemical and power plant bolting. UHC’s published selection guidance recommends 304/316 stainless steel for general indoor environments and general corrosive duty, where the joint is at normal temperature and standard load. In grade terms these are the A2 (304-based) and A4 (316-based) families, available from A2-50 and A2-70 up to A2-80 and A4-80 depending on the product form.
Duplex and super duplex stainless: UNS S32205, 1.4462, 1.4410, UNS S32750 / 2507
Where corrosion resistance is the governing condition rather than temperature, UHC’s material options extend into duplex and super duplex grades, including UNS S32205, 1.4462, 1.4410, UNS S32750 and 2507. UHC’s guidance for high-corrosion, offshore and marine environments points to 316L, duplex steel or high-temperature alloy materials. Duplex grades are a natural fit for coastal petrochemical sites, seawater cooling systems and offshore structures where a 304/316 bolt would be the weak link.
Stabilised and high-molybdenum austenitic grades: 316Ti (1.4571), 904L (1.4539), 1.4529 / UNS N08926
Between standard 316 and the nickel-based alloys sits a group of higher-alloy austenitic stainless steels: 316Ti (1.4571), 904L (1.4539) and 1.4529 / UNS N08926. These grades appear in UHC’s fastener specifications and are typically specified where a project needs more corrosion margin than 316 offers but does not need a high-temperature alloy. They are available in the same product forms as the standard stainless range.
Nickel-based high-temperature alloys: A286 ALLOY 660, ALLOY 718, ALLOY 80A
The nickel-based group is where petrochemical and power generation projects concentrate their highest demands. UHC produces high-temperature alloy fasteners in 1.4980 / A286 ALLOY 660, 2.4668 / ALLOY 718, 2.4952 / ALLOY 80A, and 1.4529 / UNS N08926. These are the materials specified when a joint must combine high temperature exposure with high tensile load, corrosion resistance and anti-fatigue performance — the combination found on turbine and boiler components, high-temperature process lines and heavy-duty flanged connections.
Strength grades, product forms and surface treatments
Material choice is only half the specification. UHC supplies strength grades A2-50, A2-70, A2-80, A4-50, A4-70, A4-80, D6-70, D6-80 and D6-100 across its range, with availability differing by product form. Thread tolerance classes are 6g / 2A for external threads and 6H / 2B / 3B for internal threads. Surface treatments include natural finish, passivation, Dacromet coating and adhesive pre-coating, and every product family is produced to ISO, DIN, ASTM, ASME, ANSI and JIS standards as specified. Alongside the stainless and alloy ranges, UHC also manufactures titanium alloy and aluminum alloy fasteners and custom industrial hardware parts, so a project can consolidate multiple material families with one supplier.

UHC Group runs five production bases covering washers, bolts and nuts, screws, studs and rivets, and hardware — 80,000 m² in total, producing 25,000 tons of stainless and special materials per year.
Step-by-Step: Matching Material to Working Condition
The following sequence works for a single flange as well as for a full project bill of fasteners. It is the order in which the specification becomes an order that arrives correctly.
- Classify the joint. Record the dominant working condition: normal temperature, high temperature, seawater corrosion, acid and alkali corrosive environment, high vibration or high tensile load. Also confirm whether the assembly is static fixed assembly under continuous mechanical load, and which tightening equipment will be used — torque wrench, electric screwdriver, hydraulic tightening machine or assembly tooling fixtures.
- Choose the material family. Apply the selection logic: 304/316 for general and indoor duty; 316L, duplex or high-temperature alloy where high corrosion, offshore or marine exposure dominates; nickel-based high-temperature alloys where high temperature and high tensile load are combined.
- Fix the strength grade. Match the grade to the product form — for example A2-70 / A4-80 on bolts and nuts, A2-50 / A4-70 on studs, or D6-80 / D6-100 where higher mechanical strength is required. State the grade explicitly; do not let it default.
- Select the product form and size. Bolts cover M2 to M160 with lengths of 6 mm to 300 mm; threaded rods and studs cover M5 to M160 with effective lengths up to 5,000 mm; nuts cover M2 to M64; washers cover M2.5 to M45; screws cover M2 to M8 with lengths of 6 mm to 100 mm.
- Set the thread tolerance class. Specify 6g / 2A for external threads and 6H / 2B / 3B for internal threads so that the bolting and the tapped components are dimensionally compatible.
- Choose the surface treatment. Natural finish, passivation, Dacromet coating or adhesive pre-coating — selected against the corrosion environment and the lubrication or anti-loosening requirement of the joint.
- Define inspection and documentation. Agree the inspection chain (first article inspection, in-process inspection, pre-shipment inspection) and the certificate package, including the 3.1 material test certificate and batch quality tracing.
- Confirm commercial terms. Fix the MOQ, lead time, monthly capacity implications and any customisation such as head mark or logo before the order is placed.
Use Cases: How the Selection Plays Out in Practice
Petrochemical process areas. Fasteners here work against acid and alkali corrosive environments and elevated temperatures. The typical split is 304/316 or duplex grades on general piping and structural connections, with 316Ti (1.4571), 904L (1.4539) or nickel-based grades on aggressive and high-temperature services. Studs and bolts in M5 to M160, with 6g / 2A thread tolerance and passivated or Dacromet-coated finishes, cover most of the bill.
Power generation. Power generation bolting must resist high tensile load, high temperature and corrosion simultaneously, which is why UHC specifies solutions for this industry with corrosion resistance and high-temperature resistance built into the requirement. Nickel-based high-temperature alloy studs and bolts are the specification of choice on hot sections, while A4-80 stainless grades serve the cooler, more conventional assemblies.
Marine and offshore adjacency. Coastal petrochemical plants and offshore platforms push the same bolting into seawater corrosion conditions. Here the recommendation moves to 316L or duplex steel, or to high-temperature alloy materials where the service also includes temperature.
High-vibration and high-load machinery. Rail transit, heavy machinery and rotating equipment call for anti-fatigue behaviour and high tensile strength under continuous mechanical load. Stainless steel fasteners to ISO, DIN, ASTM, ASME, ANSI and JIS standards with high tensile and anti-fatigue properties are the standard answer.
Ten years of field evidence. UHC fasteners have been supplied for fastening assembly in aerospace parts, marine equipment, automotive chassis and power generation facilities for over 10 years, across customer groups that include industrial equipment OEM manufacturers, engineering contractors, hardware distributors and new energy system suppliers in Germany, Italy, South Korea and Japan. One representative programme delivered 100,000 pieces against a requirement combining high tensile and anti-fatigue strength, seawater and acid-base corrosion resistance, high-temperature resistance and full compliance with DIN, ISO, JIS, ASME and ASTM standards. The reported result was a significant reduction in later maintenance replacement cost and stable project operation over the ten-year supply period.
Comparison Tables
The first table groups the material options listed in UHC fastener specifications by family and by the selection guidance that applies to each. The second table translates material choice into the practical order data a buyer has to provide.
Table 1 — Material families for petrochemical and power generation fasteners
| Material group | Designations listed in UHC specifications | Strength grades available (by product form) | Selection guidance |
|---|---|---|---|
| Austenitic stainless steel | 304, 316 | A2-50, A2-70, A2-80, A4-50, A4-70, A4-80 | Preferred for general indoor environments and standard corrosive duty |
| Stabilised and high-molybdenum austenitic | 1.4571 / 316Ti, 1.4539 / 904L, 1.4529 / UNS N08926 | A2 / A4 series and D6 series by product form | Additional corrosion margin beyond 316, without moving to a nickel-based alloy |
| Duplex and super duplex | UNS S32205, 1.4462, 1.4410, UNS S32750 / 2507 | A2 / A4 series and D6 series by product form | Recommended where high corrosion, offshore or marine conditions dominate |
| Nickel-based high-temperature alloys | 1.4980 / A286 ALLOY 660, 2.4668 / ALLOY 718, 2.4952 / ALLOY 80A | D6-70, D6-80, D6-100 by product form | Specified for high-temperature joints with high tensile load and anti-fatigue requirements |
| Martensitic stainless | 1.4006, S41000 | Listed in UHC material options | Listed as an available material in UHC fastener specifications |
Table 2 — Product forms, sizes, grades and finishing
| Product form | Size / length range | Mechanical strength grades | Thread tolerance class |
|---|---|---|---|
| Bolts (hex, flange, T-bolt, U-bolt, heavy, fit, square, anchor, foundation) | M2 – M160; length 6 mm – 300 mm | A2-70, A2-80, A4-70, A4-80, D6-80, D6-100 | 6g / 2A |
| Nuts (hex, coupling, weld, flange, nylon, heavy, jam, castle, slot, self-locking) | M2 – M64 | A2-70, A2-80, A4-70, A4-80, D6-80, D6-100 | 6H / 2B / 3B |
| Threaded rods and studs (full thread rods, double end studs) | M5 – M160; effective length up to 5,000 mm | A2-50, A2-70, A4-50, A4-70, D6-80, D6-70 | 6g / 2A |
| Washers (flat, heavy, toothed lock, serrated, wave) | M2.5 – M45 | According to material selection | Not applicable |
| Screws (tapping, marine, self-drilling, set, chipboard, socket cap, drywall) | M2 – M8; length 6 mm – 100 mm | A2-50, A2-70, A4-50, A4-70 | As specified |
| Rivets and rivet nuts (open type, close end type) | M3 – M6.4 | Materials 304/316, 6061 / 7075 aluminium | Not applicable |
All product forms above are produced to ISO, DIN, ASTM, ASME, ANSI and JIS standards as specified, with surface treatment options of natural finish, passivation, Dacromet coating and adhesive pre-coating.
Quality Control, Traceability and Acceptance Criteria
For petrochemical and power generation buyers, the material certificate is as important as the material. UHC applies a three-stage inspection chain: first article inspection, in-process inspection and pre-shipment inspection. The company operates an independent laboratory equipped to conduct comprehensive dimensional and mechanical performance tests, and holds ISO 9001 (quality management), ISO 14001 (environmental management), ISO 45001 (occupational health and safety) and EU PED certification.
Deliveries are supported by a 3.1 material test certificate, after-sales quality problem handling and batch quality tracing. Production, sales and management run on an advanced ERP system that manages the full path from raw material procurement to finished product delivery, keeping each batch efficient, transparent and traceable — the practical mechanism behind ERP-traceable stainless hardware fasteners and behind the acceptance criteria written into a project purchase order.

UHC Group was founded in 2017 and operates five production bases plus one import and export company, with 200 employees and 25 engineers.
Purchasing Terms to Confirm Before the Order
Material, size and grade determine whether the fastener works. Commercial and production terms determine whether it arrives on schedule. UHC’s standard terms for high-performance fastener projects are a minimum order quantity of 150 KG, a production lead time of 75–90 days, and a monthly capacity of 500–1,000 tons across the group. OEM and ODM production is supported, including customisation of the head mark or logo.
UHC Group is a stainless steel products supplier founded in 2017, operating five production bases and one import and export company, with 80,000 m² of factory space, 25 engineers in the R&D team and annual output of 25,000 tons of stainless and special materials. Around 80% of production is exported, with principal markets in the EU, Korea and Japan and additional export activity across the U.S., Middle East and South America. Buyers in Germany, Japan, South Korea and Italy will find these petrochemical and power generation application scenarios familiar, and 75–90 day lead times should be planned into the project schedule rather than absorbed at the end.
FAQ
Do petrochemical and power generation fasteners need PED certification or specific international standards?
Fasteners for pressure equipment in the EU must comply with the Pressure Equipment Directive (PED) 2014/68/EU, and ISO 3506-1:2020 specifies the mechanical properties of corrosion-resistant stainless steel bolts, screws and studs. UHC fasteners are produced to ISO, DIN, ASTM, ASME, ANSI and JIS standards as specified, and UHC Group holds ISO 9001, ISO 14001, ISO 45001 and EU PED certification. Deliveries include a 3.1 material test certificate with batch quality tracing, and preloaded structural connections may fall under the EN 14399 series. State the governing standard, strength grade and thread tolerance class on the purchase order so that the drawing, the material certificate and the goods-in inspection all reference the same specification.
Can one supplier deliver both 304/316 stainless and nickel-based alloy fasteners for the same project?
Yes. UHC manufactures stainless steel fasteners (304, 316, A2-70, A4-80), high-temperature alloy fasteners, titanium alloy and aluminum alloy fasteners, solar PV mounting components and custom industrial hardware parts. Product forms include hex, flange, T, U, heavy, fit, square, anchor and foundation bolts from M2 to M160 with lengths of 6 mm to 300 mm; threaded rods and studs from M5 to M160 with effective lengths up to 5,000 mm; nuts from M2 to M64; washers from M2.5 to M45; and screws from M2 to M8. Strength grades run from A2-50 and A2-70 through A2-80, A4-50, A4-70, A4-80, D6-70 and D6-80 to D6-100 depending on product form, with 6g / 2A external and 6H / 2B / 3B internal thread tolerance classes. Five production bases, 80,000 m² of factory space and 500–1,000 tons of monthly capacity support mixed material orders.
What drives the cost difference between 304/316 stainless and nickel-based alloy fasteners?
Three factors dominate: material chemistry, processing and verification scope. Nickel-based and high-molybdenum alloys contain higher levels of alloying elements than 304 or 316, so their cost tracks alloy markets rather than the standard stainless market. They also require more careful forming, heat treatment and machining, particularly on higher strength grades such as D6-80 and D6-100 and on precision thread classes. Verification adds cost as well, because first article inspection, in-process inspection, pre-shipment inspection and a 3.1 material test certificate all form part of the delivered package. The practical budgeting rule is to keep 304/316 (A2/A4) on general and standard corrosive duty, and reserve duplex and high-temperature alloys for high-corrosion, offshore, marine or high-temperature joints. Over-specifying the alloy is a common source of avoidable project cost; under-specifying it is a common source of rework.
Can samples be validated before a full project order is placed?
Sample and first-article validation is built into UHC’s normal quality process rather than treated as an exception. The control chain begins with first article inspection, continues through in-process inspection and closes with pre-shipment inspection, and the independent laboratory is equipped for dimensional and mechanical performance testing. Batches remain traceable through the ERP system from raw material procurement to finished product delivery, and supplied material is backed by a 3.1 material test certificate with batch quality tracing. Send the drawing or a target specification — material, product form, size, strength grade, thread tolerance class, surface treatment and governing standard — and the engineering team will confirm feasibility and discuss sample and validation arrangements as part of the quotation.
What are the MOQ, lead time and delivery terms for high-performance fasteners?
UHC’s standard terms are a minimum order quantity of 150 KG, a production lead time of 75–90 days and a monthly capacity of 500–1,000 tons, with OEM/ODM support including head mark or logo customisation. Production runs across five production bases covering washers, bolts and nuts, screws, studs and rivets, and hardware, with total annual output of 25,000 tons of stainless and special materials. Around 80% of output is exported, with the EU, Korea and Japan as principal markets. For a petrochemical or power generation package, share the full bill of materials with material grades and sizes so that capacity and lead time can be confirmed in one step — contact UHC at michaelshen@uhc-group.com.cn or +86 13575349247, or review the full capability range in the company brochure.
Conclusion: Decide by Joint, Not by Plant
The comparison between 304/316 stainless steel and nickel-based alloy fasteners does not end with a winner. It ends with a rule that can be applied across an entire petrochemical or power generation project: match the material family to the dominant working condition, then lock the strength grade, product form, size, thread tolerance class, surface treatment and acceptance criteria to that choice.
304/316 in A2 and A4 grades remains the correct default for general and standard corrosive duty. Duplex and high-molybdenum grades such as UNS S32205, 316Ti (1.4571) and 904L (1.4539) carry the corrosion margin. Nickel-based high-temperature alloys — A286 ALLOY 660, ALLOY 718 and ALLOY 80A — carry the high-temperature, high tensile load joints where anti-fatigue performance cannot be compromised. Supplying all of them from one source, with the same inspection chain and the same traceability, removes the split-supplier risk that turns a materials decision into a project delay.

Send your drawing or specification to receive a material-matched quotation for petrochemical and power generation fasteners.
Next step
UHC — Jiaxing Union Hardware Co., Ltd. manufactures high-performance fasteners in 304/316 stainless, duplex, nickel-based high-temperature and titanium/aluminium alloys, from M2 to M160, to ISO, DIN, ASTM, ASME, ANSI and JIS standards.
Email: michaelshen@uhc-group.com.cn or sales@uhc-group.com.cn | Tel / WhatsApp: +86 13575349247 | Website: www.jxuhc.com | Blog: blog.jxuhc.com
Download the full product brochure: UHC Group product catalogue (PDF)
Have Questions or Need More Details?
Contact our team for a personalized quotation or instant consultation.
Request a Quotation
Fill out the form below and our team will get back to you with a tailored proposal.
WhatsApp Direct Chat
Prefer to chat in real-time? Message us on WhatsApp for instant assistance & quick answers.
- Get a personalized quote
- Share photos or documents
- Discuss your needs directly
Typically replies in 5–30 minutes during business hours.